
Flight-Critical Precision & Extreme-Environment Engineering
From multi-axis simultaneous CNC machined titanium blisks to topology-optimized satellite airframes and superalloy propulsion manifolds — BoValley delivers flight-ready aerospace manufacturing compliant with AS9100D and ISO 9001 quality management systems.
Case 01 | 5-Axis CNC Titanium Turbine Impeller (Aerospace Blisk / Closed Impeller)
Multi-Angle Visual Gallery
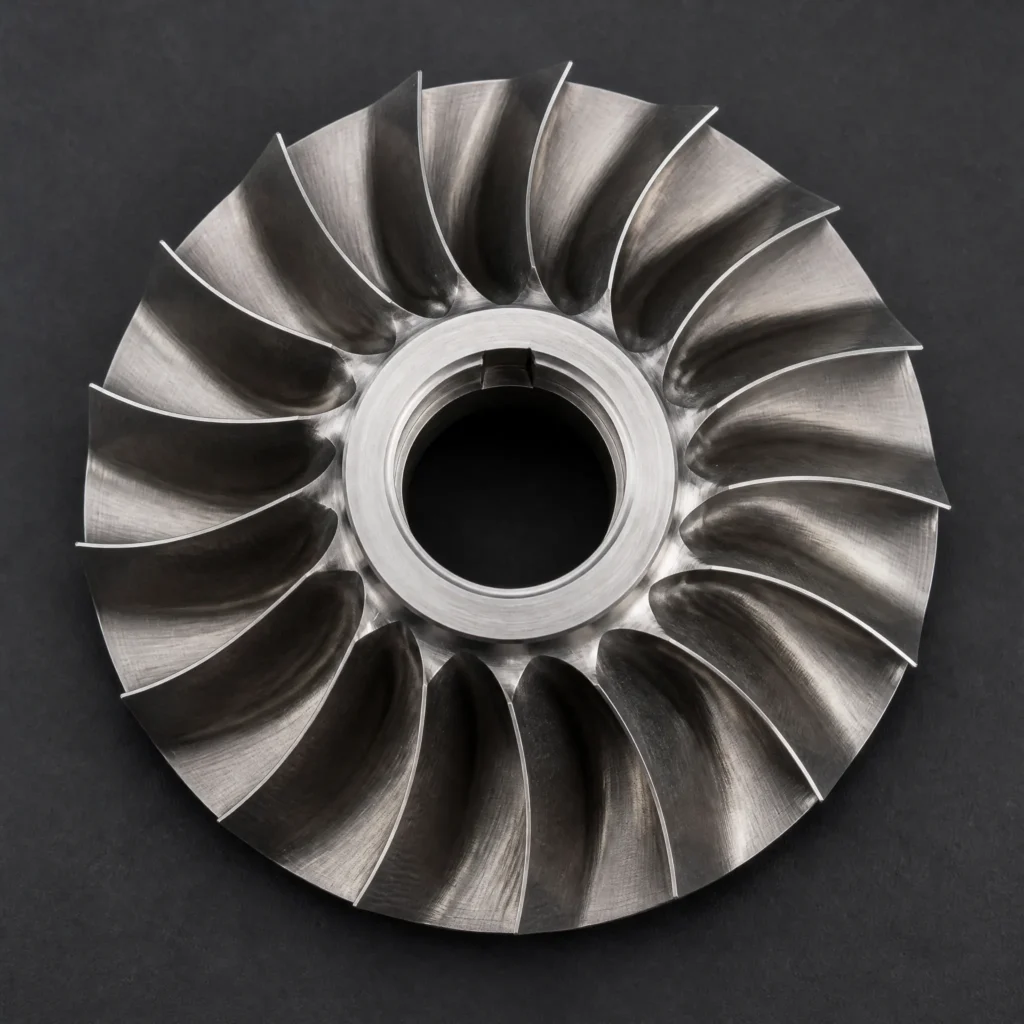
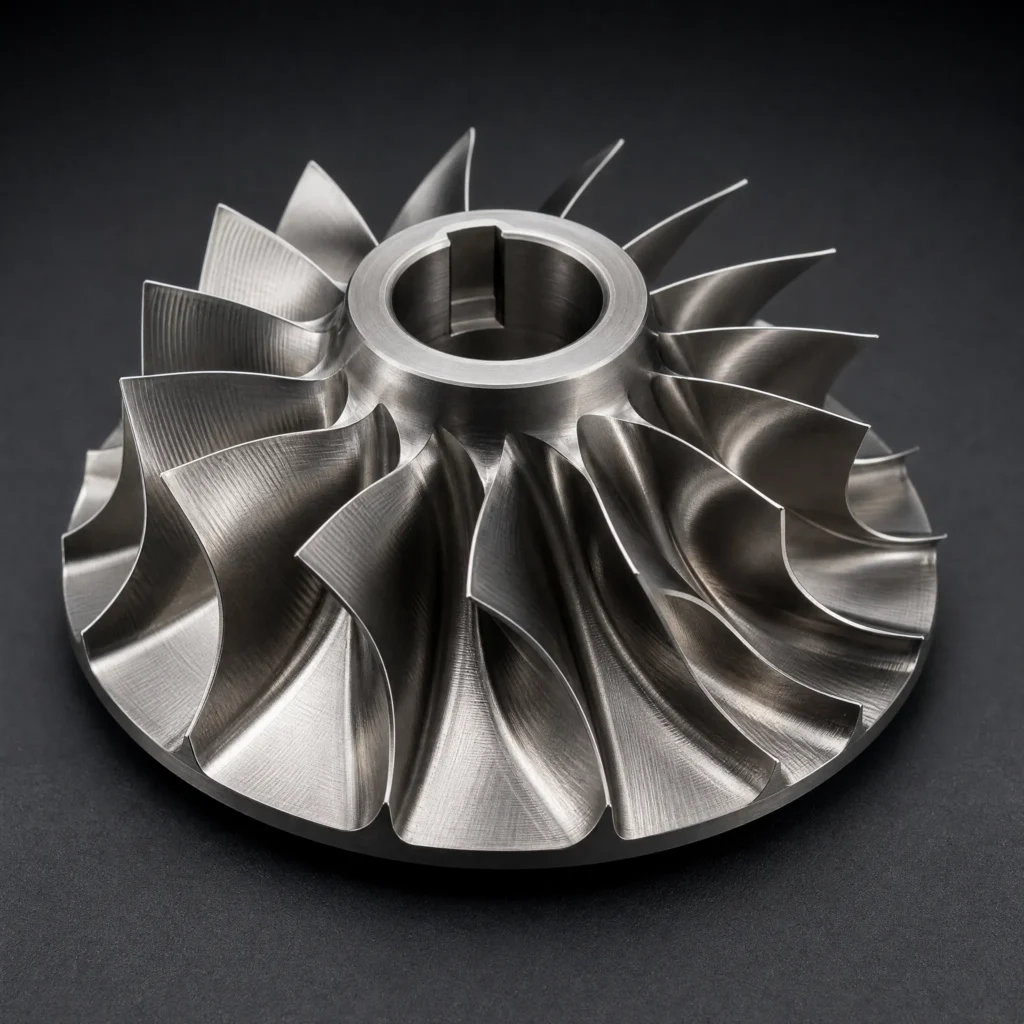

1. Manufacturing Process & Material Selection
- Core Process: 5-Axis Simultaneous CNC Machining (Continuous Toolpath Flank & Point Milling) + Micro-Abrasive Flow Machining + Dynamic Balancing + Fluorescent Penetrant Inspection.
- Material Grade: Aerospace-Grade Titanium Alloy Ti-6Al-4V (Grade 5 / AMS 4928)
- Engineering Justification: Extraordinary strength-to-density ratio (≈4.43 g/cm3), high fracture toughness, and superior creep/corrosion resistance at operating temperatures up to 400℃.
- Tolerances & Surface Finish: Blade aerodynamic profile contour tolerance within ±0.010 mm; central bore concentricity ≤0.005 mm; gas-flow channel surface roughness polished to Ra 0.2–0.4μm.
2. Structural Features & Manufacturing Challenges
- Ultra-Thin Twisted Aerodynamic Blade Geometry:
- Challenge: Blade trailing edge thickness thins down to 0.6mm over an extended curvature. High cutting forces induce blade deflection, chatter vibration, and harmonic distortion during multi-axis simultaneous flank milling.
- Solution: Utilized custom tapered solid-carbide ball end-mills with specialized AlTiN coatings, synchronized with synchronized 5-axis adaptive trochoidal toolpaths. Maintained mirror-image dual-blade balanced milling sequences while injecting soluble polymer dampening backing to eliminate blade flexure.
- Deep Hub Pocketing & Tool Interference Prevention:
- Challenge: Narrow flow channels between adjacent twisted blades create extreme tool clearance constraints and spindle collision risks.
- Solution: Conducted full kinematic collision simulation in hyperMILL CAM software, leveraging continuous tool-axis tilting vectors to ensure optimal cutter contact point without gouging adjacent aerofoils.
3. Real-World Applications
- Auxiliary Power Units (APU) & Micro-Turbojet Compressors: Delivering high-pressure ratio compression stages for commercial and regional aviation propulsion.
- Aerospace Environmental Control Systems (ECS): Powering high-speed cabin pressurization air cycle turbines and avionics cooling expanders.
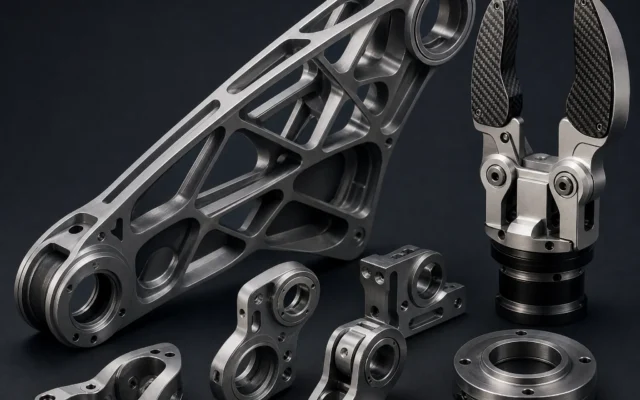
Case 02 | Aerospace Satellite Structural Bracket (Topology-Optimized Primary Airframe Mount)
Multi-Angle Visual Gallery
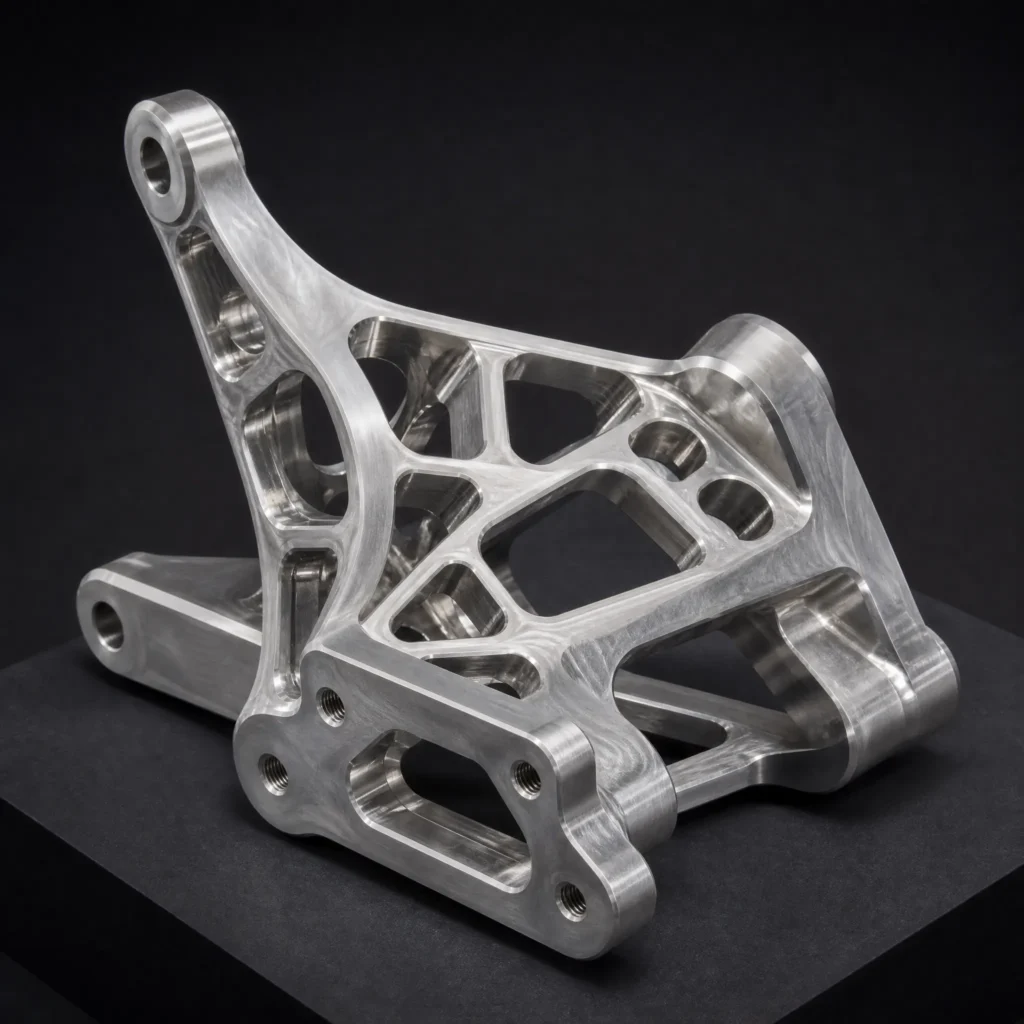
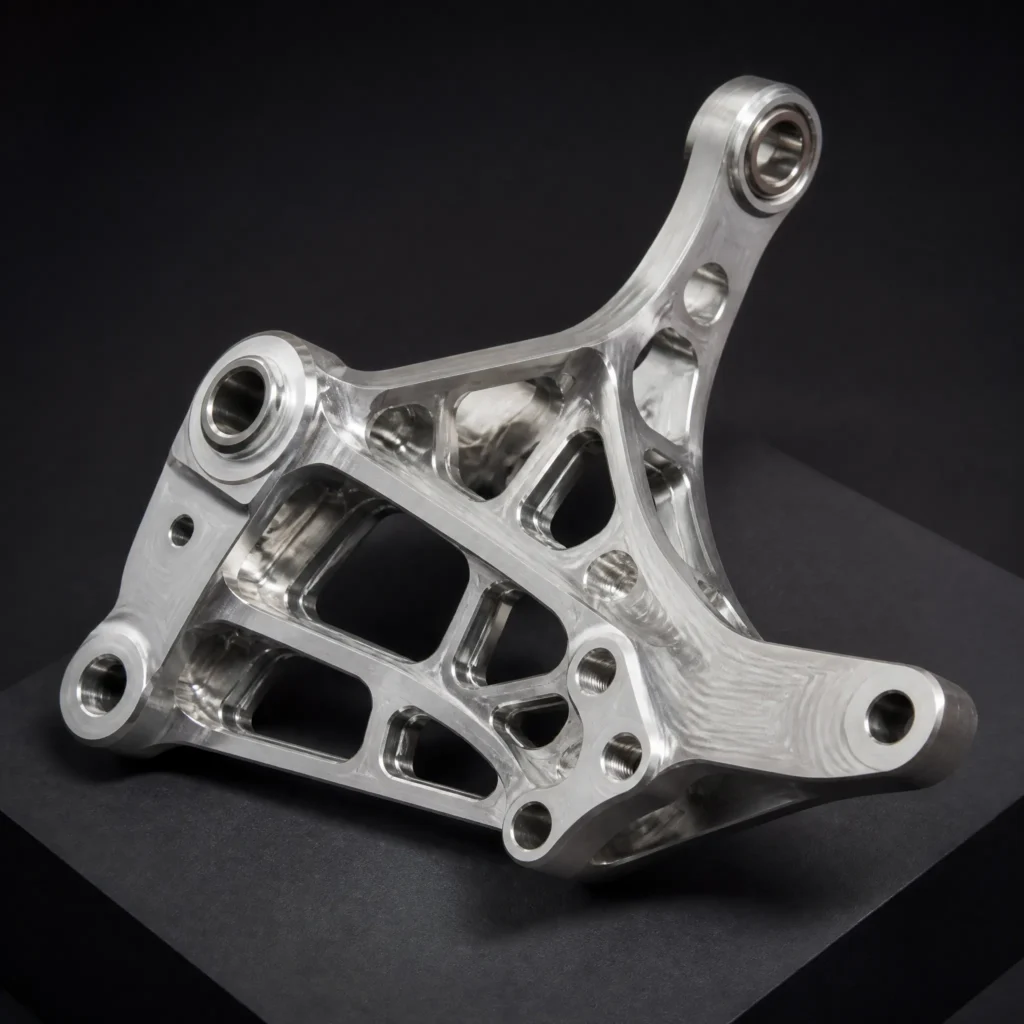
1. Manufacturing Process & Material Selection
- Core Process: High-Speed 5-Axis CNC Milling Center (30,000 RPM Spindle) + Cryogenic Machining Assist + Stress-Relief Thermal Annealing + Sulfuric Acid Anodizing with PTFE Sealing (MIL-A-8625 Type II).
- Material Grade: Aerospace Aluminum Alloy 7075-T651 (AMS 4045) / Al-Li 2195
- Engineering Justification: Ultra-high yield strength (≥505 MPa), high modulus of elasticity, and stress-relieved stretching (T651 temper) for extreme dimensional stability across launch vibration and orbital thermal cycles (−150℃ to +120℃).
- Tolerances & Precision: Pivot spherical bearing bore tolerance held to ±0.006 mm; mounting plane flatness over 380 mm span kept within ≤0.015 mm.
2. Structural Features & Manufacturing Challenges
- Excessive Material Removal Rate (>85%) & Distortion Mitigation:
- Challenge: Monolithic machining from a solid forged block releases locked-in residual quenching stresses, causing severe free-state warping and twisting.
- Solution: Adopted a multi-stage roughing sequence alternating between opposing faces to symmetrically peel away material. Performed intermediate cryogenic cryogenic treatment (sub-zero stabilization at −80℃), followed by semi-finish and final finish clamping under zero-stress vacuum chucks.
- Deep Pocket Pocketing with Thin Ribs (1.2 mm):
- Challenge: Tall, thin structural webs are prone to deflection under cutting pressure, resulting in tapered wall errors and surface chatter.
- Solution: Deployed step-down high-feed plunge milling and corner circular ramping to maintain continuous chip load, followed by high-speed light-skim finishing passes.
3. Real-World Applications
- Low-Earth Orbit (LEO) Satellite Solar Array Hinge Bracket: Primary mechanical interface carrying the deployable solar wing deployment loads and satellite bus integration points.
- Flight Control Surface Actuator Linkage: High-load mechanical mounting brackets for aircraft flap/rudder electro-mechanical actuation systems.
See the processes, materials and inspection considerations for aerospace manufacturing at BoValley.