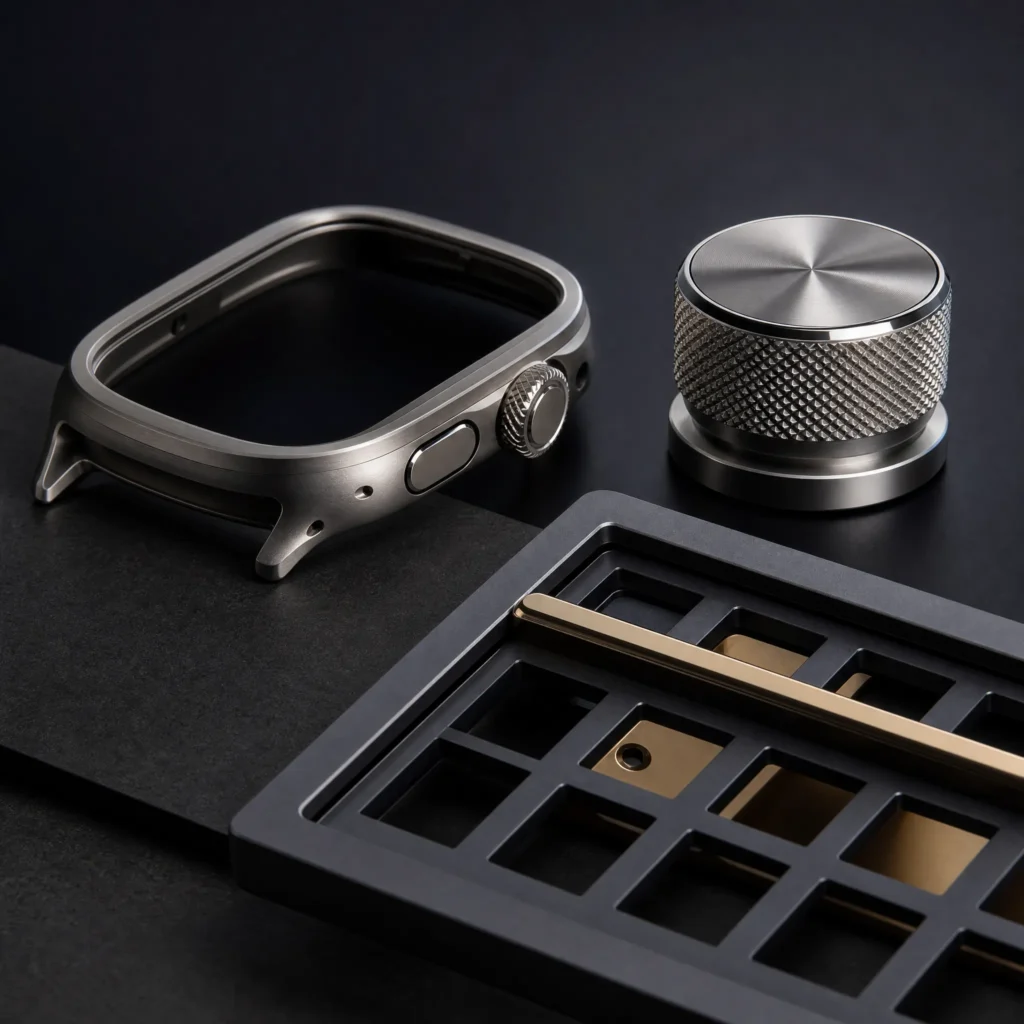
BoValley provides rapid prototype development and volume CNC / injection molding production for consumer electronics leaders, smart wearable pioneers, and spatial computing innovators. Utilizing high-speed micro-milling(45,000 RPM), automated multi-axis robotic buffing, ultra-fine bead blasting, and automated colorimetry anodizing, we transform complex industrial design concepts into premium, production-ready consumer products.
Case 01 | Wireless Earbuds Charging Case Unibody Metal Frame
Multi-Angle Visual Gallery
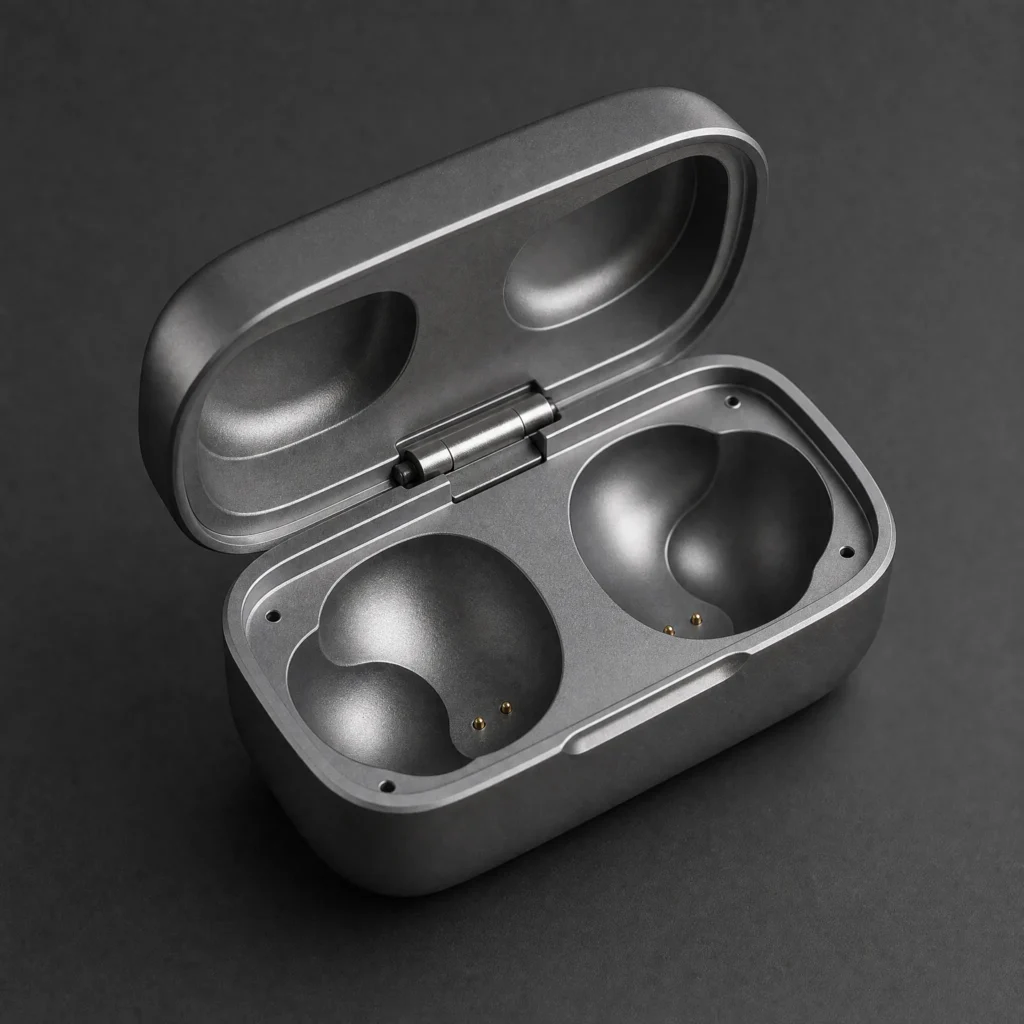
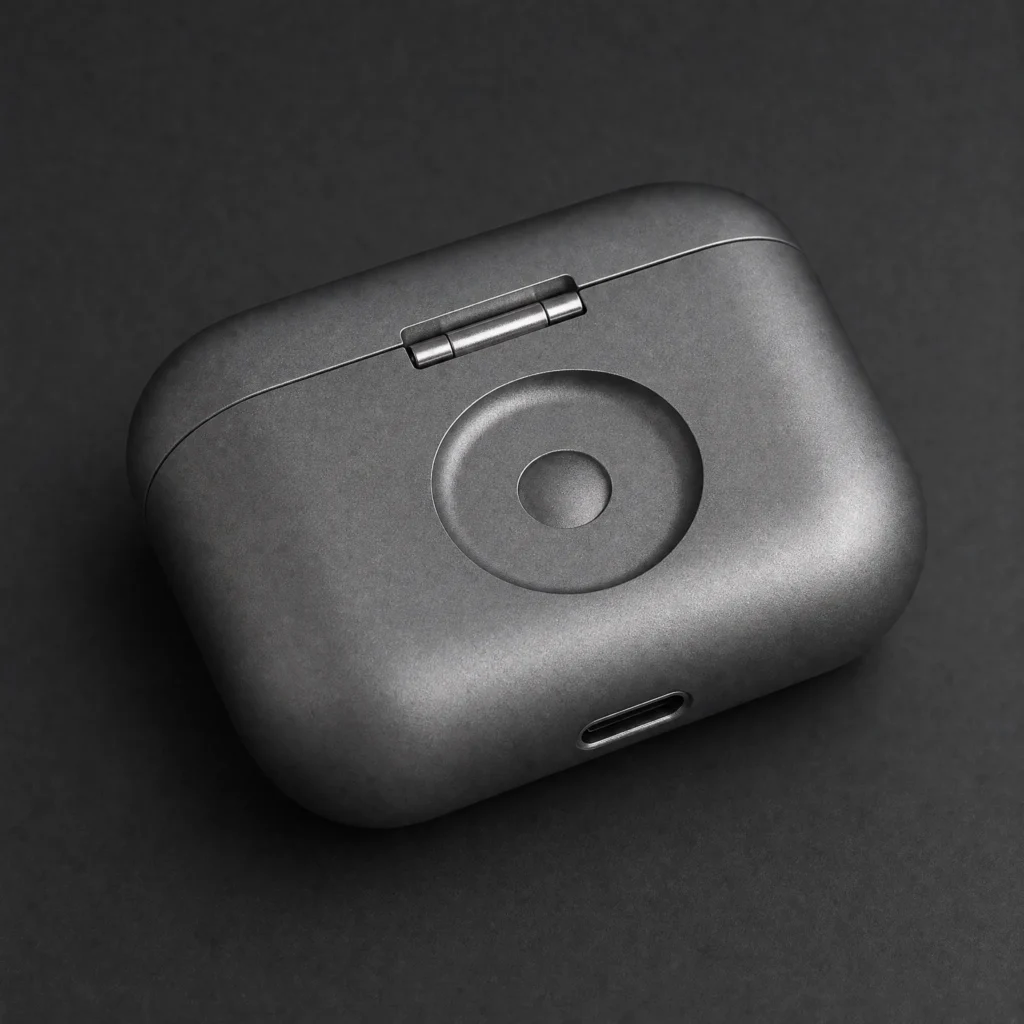
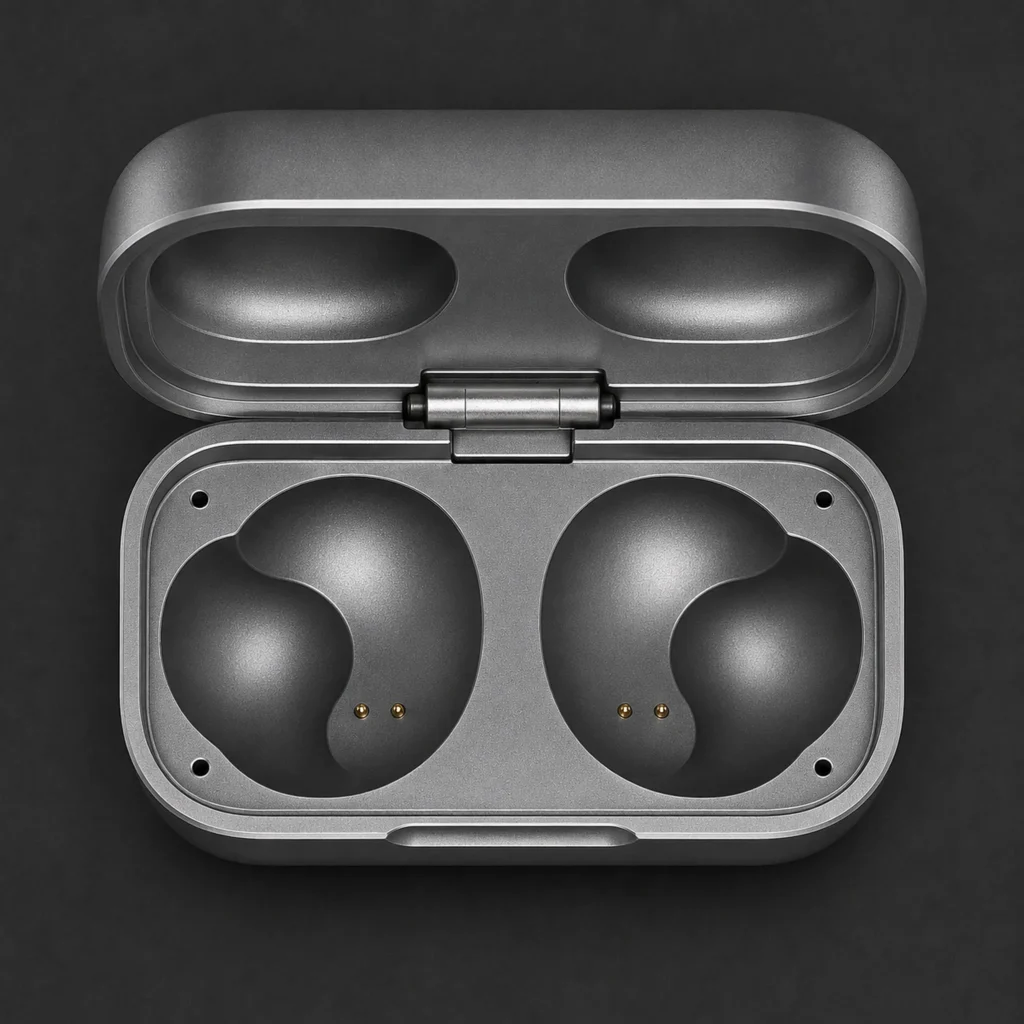
1. Manufacturing Process & Material Selection
- Core Process: High-Speed Multi-Axis CNC Milling (45,000 RPM Spindle) + 3D Automated Robot Buffing & Polishing + 220# Ceramic Bead Blasting + Magnetic High-Uniformity Color Anodizing (Space Grey).
- Material Grade: High-Purity Extruded Aluminum Alloy 6063-T6
- Engineering Justification: Superb anodizing clarity with zero streak defects, excellent ductile impact resistance against floor drops, and premium thermal dissipation.
- Tolerances & Aesthetics: External 3D curvature profile tolerance ±0.015 mm; thin-wall battery pocket thickness 0.60±0.02mm; color delta E≤0.5 across production batches.
2. Structural Features & Manufacturing Challenges
- Ultra-Thin Deep Cavity Milling with Zero Chatter:
- Challenge: The internal battery and earbud cavities are deeply hollowed, leaving peripheral wall thicknesses of only 0.6mm. High-speed milling easily causes tool chatter, thin-wall vibration waviness, and deformation.
- Solution: Designed dedicated low-melting-point alloy (or high-adhesion vacuum ice-chuck) internal casting fixtures that support the thin walls during external 3D contour finishing.
- Zero-Gap Micro-Hinge & Magnetic Latch Integration:
- Challenge: The spring-loaded hinge cutout requires zero-gap aesthetic alignment with the lid, leaving no visible cutter step-overs.
- Solution: Executed micro-radius corner machining using 0.3mm diamond-coated end mills, finishing cosmetic edges with automated multi-axis robotic abrasive paste polishing.
3. Real-World Applications
- Flagship Active Noise Cancelling (ANC) Earbuds Cases: Providing structural rigidity, drop protection, and premium metallic in-hand tactile feel.
- Smart Ring & Wearable Sensor Wireless Charging Docks: Precision charging pods with integrated magnetic pogo-pin contacts.
Case 02 | Ultra-Slim Laptop Unibody Enclosure (C-Cover Keyboard Deck)Multi-Angle Visual Gallery
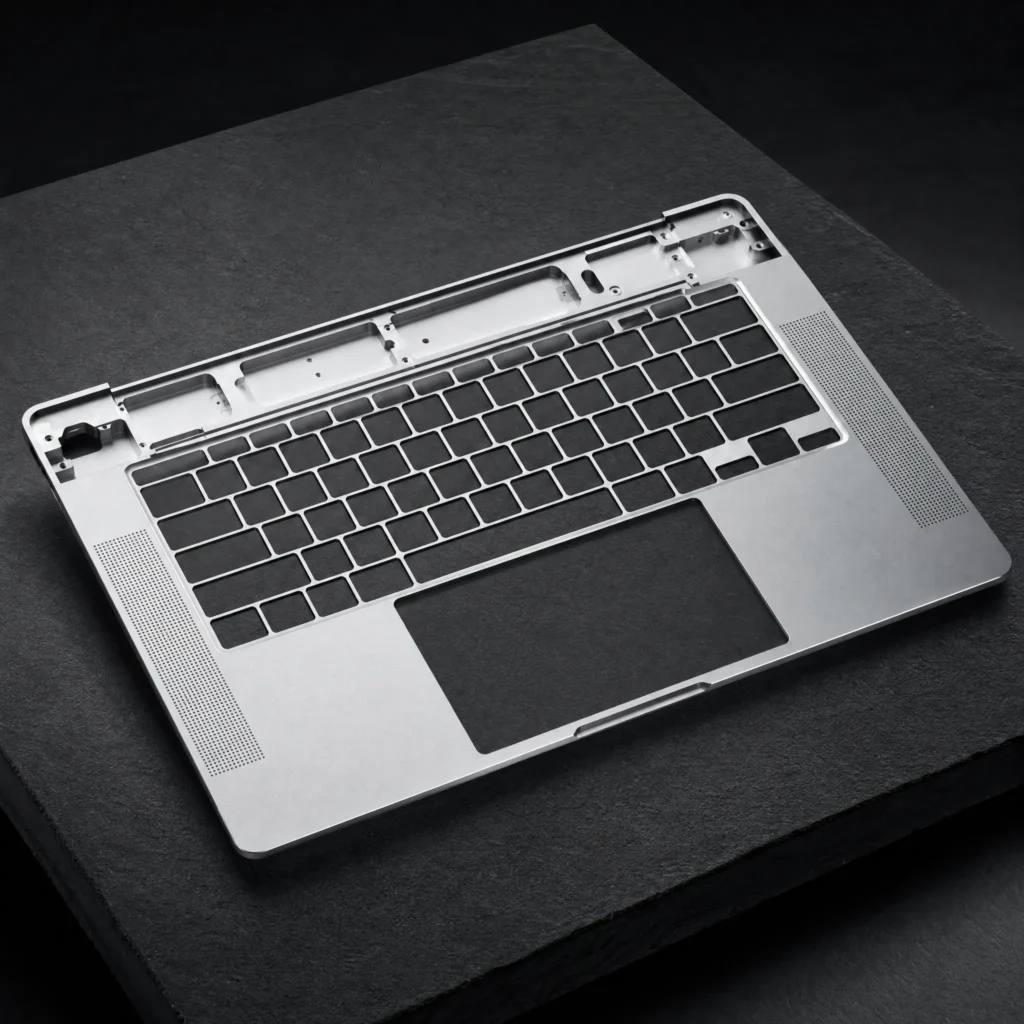
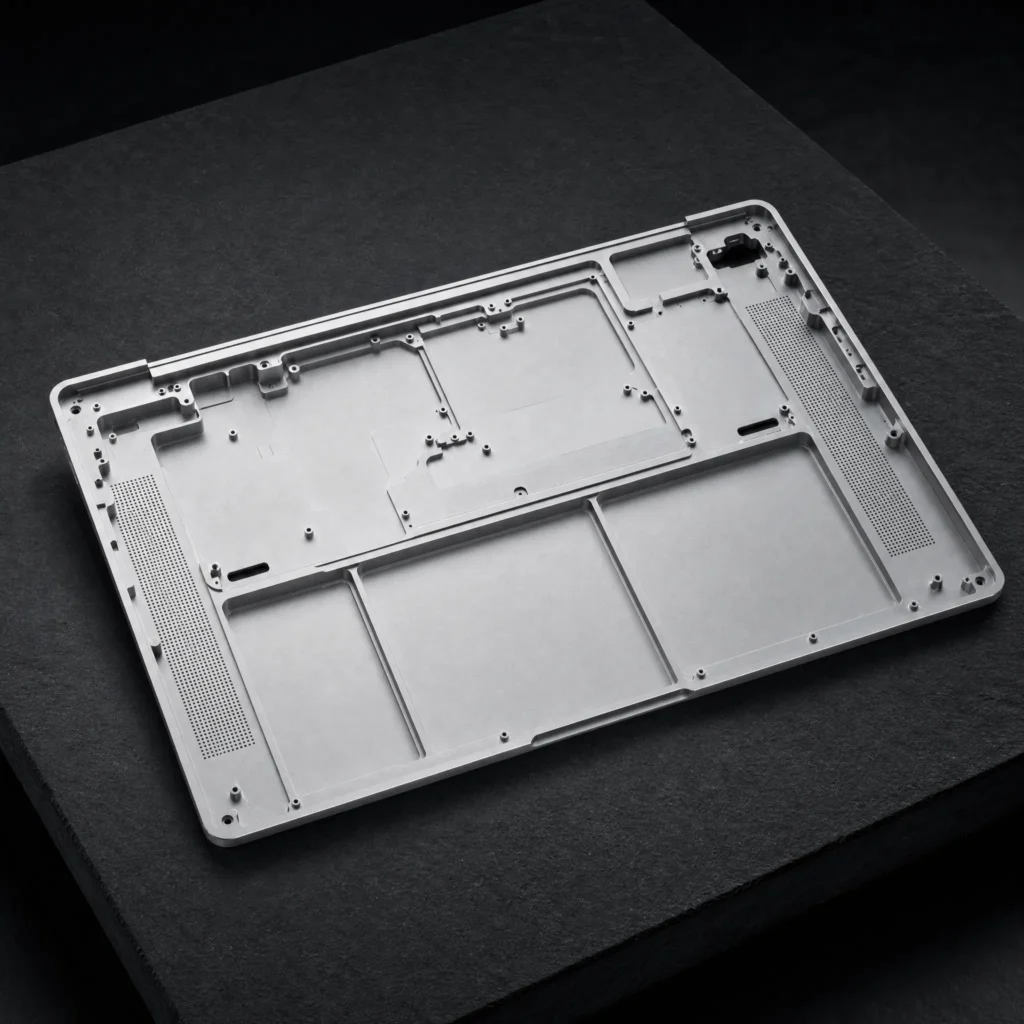
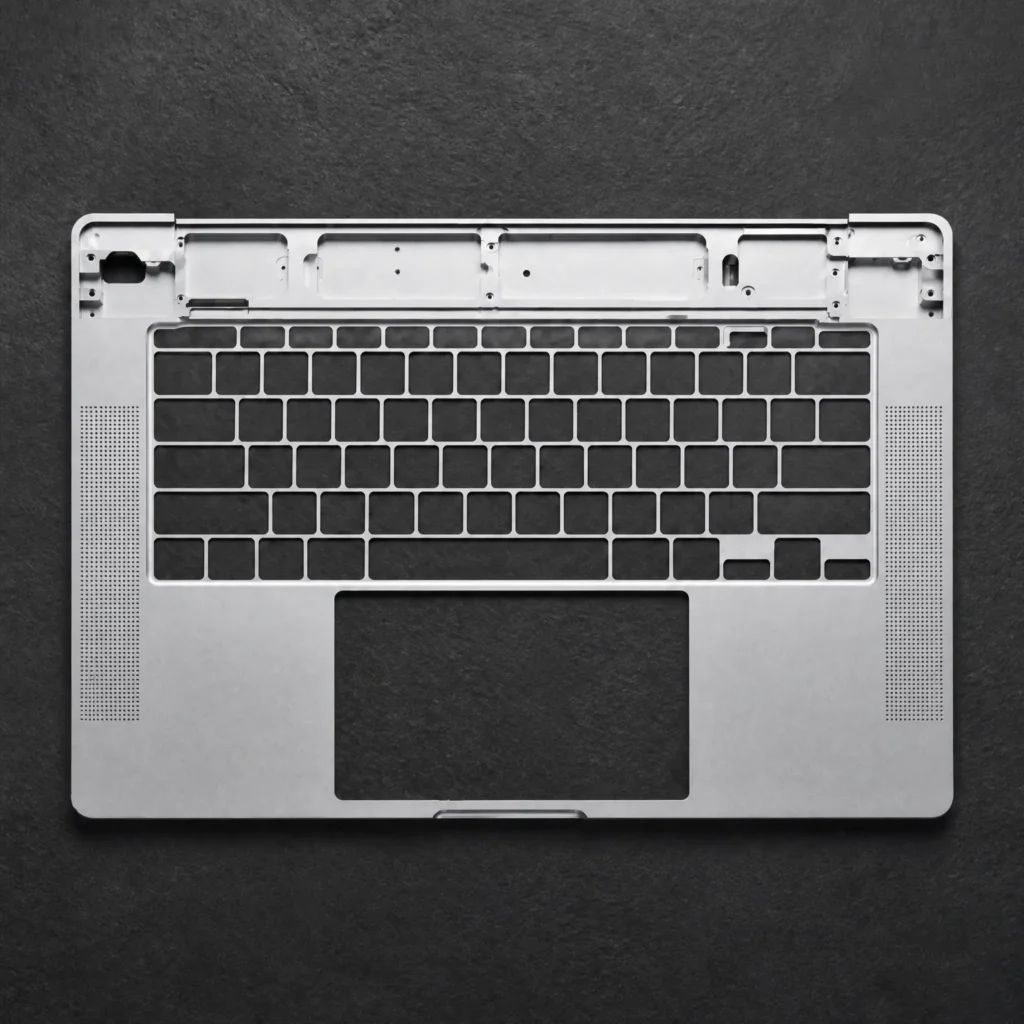
1. Manufacturing Process & Material Selection
- Core Process: Large-Format Gantry High-Speed CNC Machining Center (25,000 RPM) + Micro-Perforation Laser/Drilling + Dual-Face Symmetrical Milling + Stress-Relief Thermal Leveling + 180# Micro-Bead Blasting & Satin Anodize.
- Material Grade: Aviation-Grade Aluminum Alloy 6013-T6 / 6061-T651
- Engineering Justification: High flexural stiffness preventing keyboard flex during typing, excellent thermal spreading to channel CPU/GPU heat away from internal components.
- Tolerances & Dimensions: Overall 350mm diagonal diagonal flatness ≤0.08mm; keyboard grid web bridge thickness 0.80±0.02mm; trackpad aperture edge chamfer uniformity ±0.010mm.
2. Structural Features & Manufacturing Challenges
- Large-Aspect-Ratio Thin-Plate Warpage(1.0mm Nominal Thickness):
- Challenge: Machining from a 15mm thick solid aluminum plate to a 1.0mm monolithic shell releases internal rolling stresses, causing severe diagonal twisting.
- Solution: Developed a 4-station symmetrical machining process with intermediate stress-relief baking (180℃ for 4 hours), using porous ceramic vacuum chucks to clamp the part during final perimeter contouring.
- Acoustic Speaker Micro-Hole Array Drilling (Zero-Burr):
- Challenge: Drilling over 3,000micro-holes (∅0.4mm) through the top palm rest without any entry or exit burrs.
- Solution: High-speed micro-peck drilling spindles with diamond-coated micro-drills, followed by high-pressure deionized water deburring and electrochemical polishing.
3. Real-World Applications
- Ultra-Portable Flagship Laptops & 2-in-1 Tablets: Monolithic chassis providing keyboard support, trackpad integration, and structural drop resistance.
- High-End Creator Laptops & Industrial Field Terminals: Lightweight, rugged aluminum structural chassis housing cooling vapor chambers.
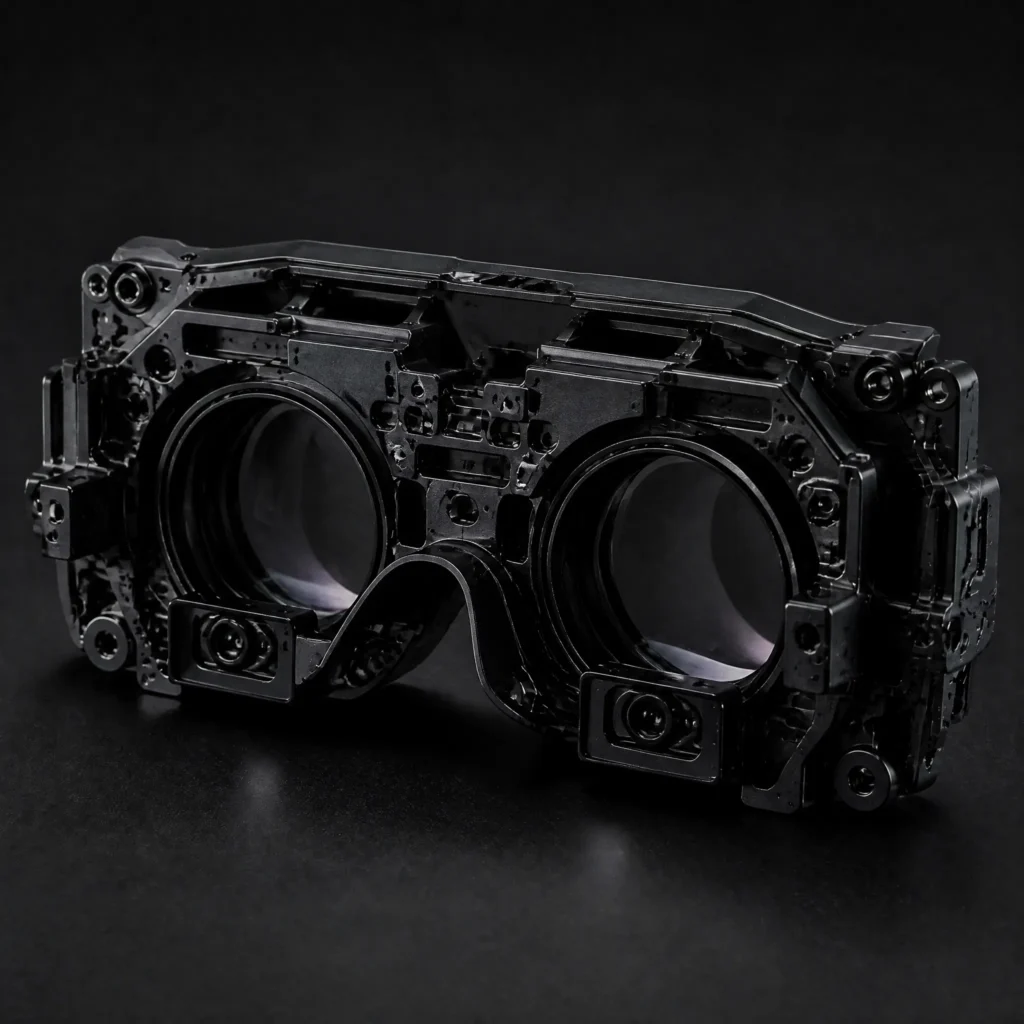
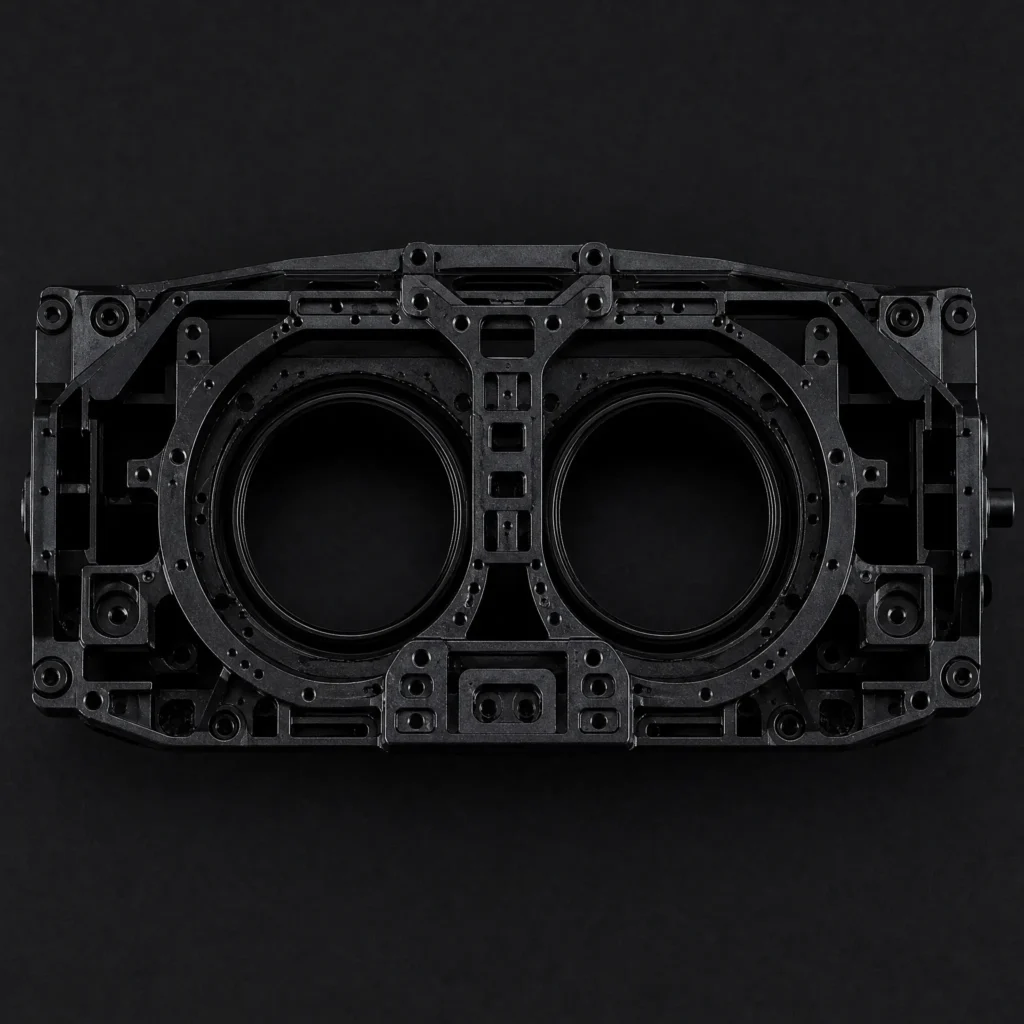
Case 03 | AR/VR Smart Headset Optical Engine Chassis (Magnesium Spatial Computing Core)
Multi-Angle Visual Gallery
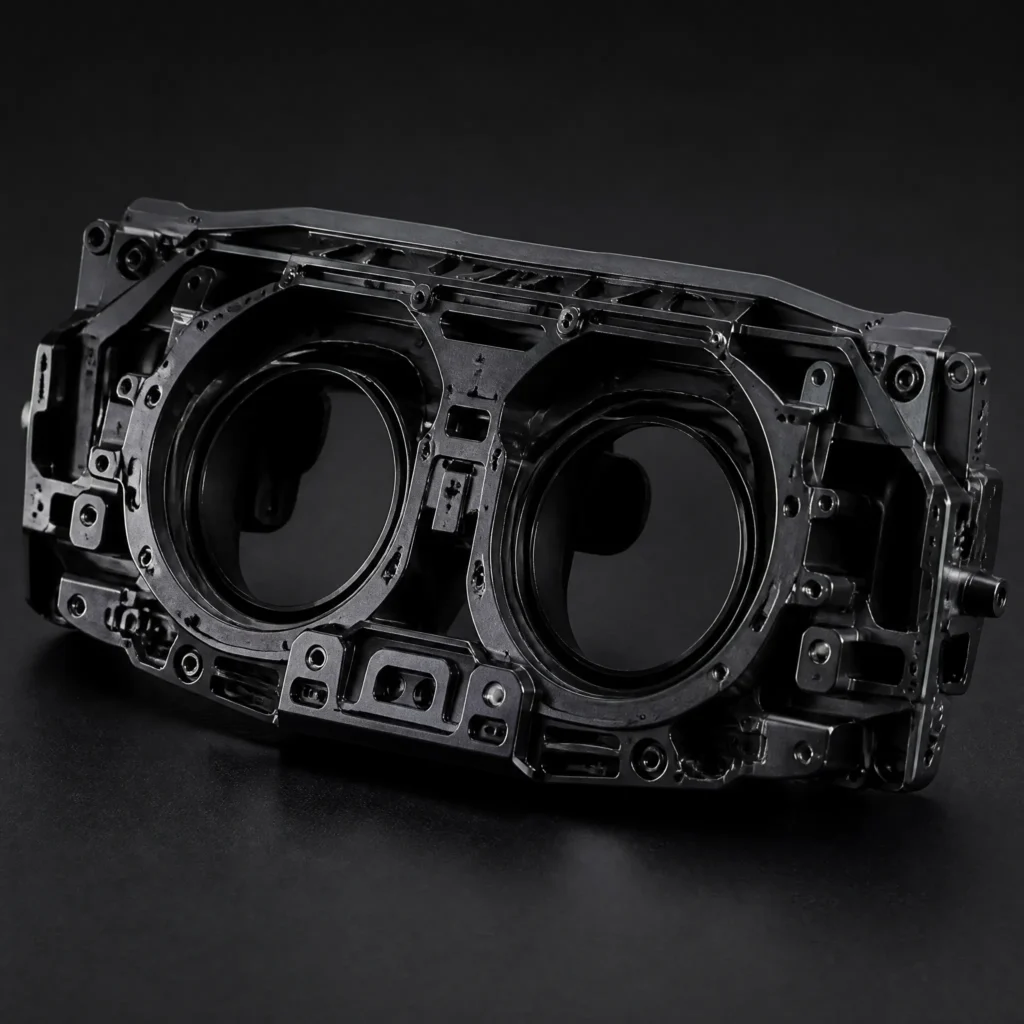
1. Manufacturing Process & Material Selection
- Core Process: 5-Axis Micro-CNC High-Speed Milling + Micro-EDM Wire Sizing + Micro-Arc Oxidation (MAO) / Deep Black Electrophoretic Deposition (EPD).
- Material Grade: Ultra-Lightweight Magnesium-Aluminum Alloy AZ91D / Al-Li Alloy
- Engineering Justification: Density is 33% lighter than aluminum (≈1.81g/cm³) to minimize front-heavy headset pressure on the user’s face, with high structural damping capacity absorbing micro-vibrations.
- Tolerances & Optical Alignment: Inter-pupillary distance (IPD) slide rail parallelism≤0.005mm; micro-OLED display mounting pocket planar flatness≤0.003mm; optical barrel seating tilt≤15 arcsec.
2. Structural Features & Manufacturing Challenges
- High-Density Miniature Skeletal Truss Machining:
- Challenge: Structural walls as thin as 0.5mm integrate display brackets,, optical lens holders, and eye-tracking camera nests, highly vulnerable to cutting heat distortion.
- Solution: High-speed micro-milling with continuous cryogenic air-blast cooling (avoiding liquid coolant fire risks with magnesium), applying dynamic toolpath optimization to maintain minimal tool contact pressure.
- Non-Reflective Light Absorption Coating on Magnesium:
- Challenge: AR/VR displays require zero internal optical bounce-back to eliminate display lens flares.
- Solution: Developed a specialized Micro-Arc Oxidation (MAO) black ceramic conversion coating that creates a micro-porous light-trapping surface with zero outgassing in sealed optical cavities.
3. Real-World Applications
- Next-Generation Spatial Computing & Mixed Reality (MR) Headsets: Forming the central rigid optomechanical frame that locks pancake lenses, micro-OLEDs, and eye-tracking cameras in sub-micron alignment.
- Smart AR Glasses & Industrial HUD Waveguide Modules: Housing ultra-compact laser beam scanning (LBS) or Micro-LED optical projection engines.
See the processes, materials and inspection considerations for consumer electronics manufacturing at BoValley.